Condensate pumps for tidy drainage on cold equipment
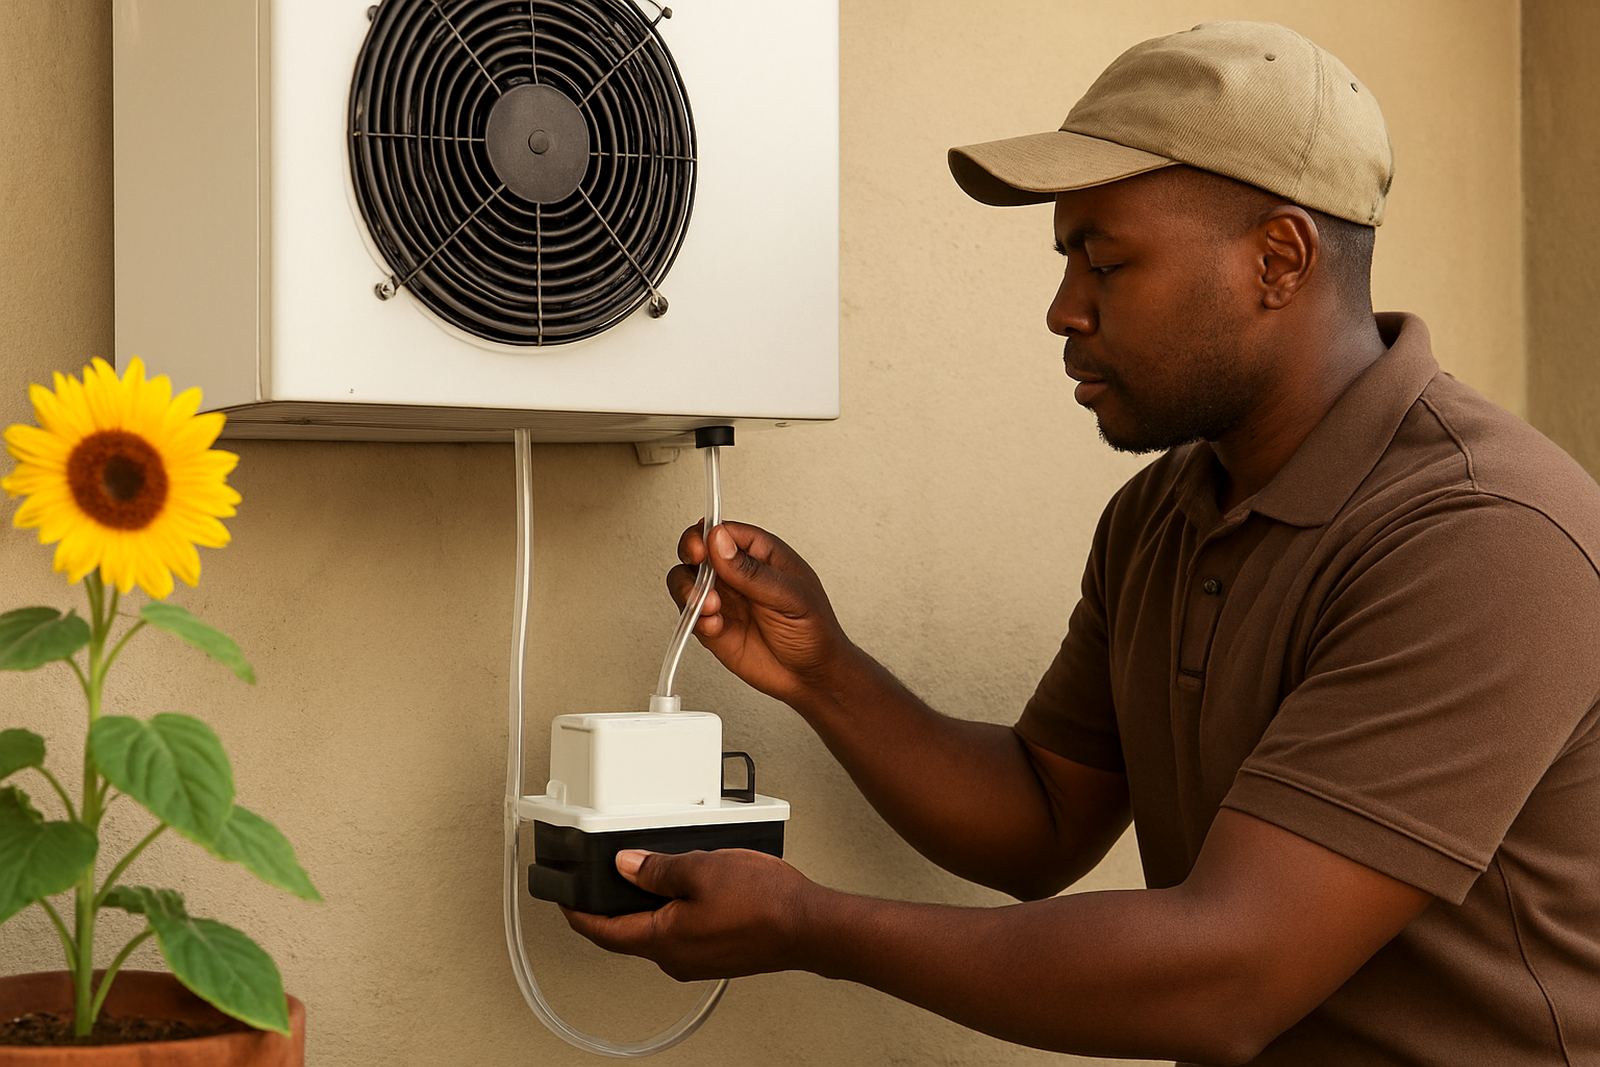
A condensate pump is a small duty pump fitted to move melt water and drip tray water from refrigeration equipment to a suitable drain point. In many cabinets and ceiling mounted evaporators, there is no easy fall to a floor waste, or the nearest drain is simply too far away. The pump takes that water away in controlled cycles, so the unit can keep working without pooling, staining or unnecessary shut downs.
For shops, butcheries, bakeries, packhouses and small cold rooms across Gqeberha and the Eastern Cape, this is a practical fix. It helps where pipe routes are tight, where the drain is higher than the unit, or where a tidy install matters in a public area. In humid coastal air, condensation can build fast, so a properly selected pump can save a lot of grief later.
Where condensate pumps suit local refrigeration jobs
These pumps are commonly used on display cabinets, undercounter chillers, evaporator drip trays, compact cold rooms and small split cooling installations. They are especially useful in Newton Park, Despatch, Uitenhage and Jeffreys Bay where older buildings may not have ideal drainage points. In some sites, the drain run has to pass through a wall, along a ceiling void or over a short rise, and that is where a pump earns its keep.
They also suit places that need cleaner floors and less slip risk. A blocked or badly routed drain can leak onto tiles, damage ceilings below, or cause smells around stock. For food areas, that is not just untidy, it can affect hygiene checks and staff safety.
- Retail fridges with limited access to floor drains
- Walk-in coolers with low drip tray discharge points
- Small packhouses and holding rooms
- Back-of-house kitchens and prep areas
- Plant rooms where water must be lifted to a higher waste line
Sizes, capacities and common options
Condensate pumps are not one-size-fits-all. The right unit depends on the amount of water generated, the lift required, the pipe run and how much space is available for the tank and pump body. Some models are compact and suited to a single cabinet, while others are better for multiple evaporators or a small cold room bank. A unit that is too small can short cycle and wear out early, while one that is oversized may be bulky and harder to fit neatly.
Typical options include a small collection tank, float switch activation, a non-return valve, a high level alarm and mounting brackets for neat installation. In some cases, a pumped discharge line with 6 mm to 8 mm hose is enough. In others, a larger bore line is better for longer runs and fewer blockages. The pump head, meaning the height it can lift water, must be checked against the actual site level, not just the brochure figure.
- Compact pump units for single cabinets or undercounter units
- Medium duty pumps for evaporators and small cold rooms
- Higher lift units for plant room and ceiling void routing
- Alarm fitted options for critical stock areas
- Tank and hose sets with mounting hardware
Installation and power checks before fitting
A good pump install starts with the drain path, the pipe route and the power supply. The unit must sit level, the inlet must drain freely, and the discharge line should avoid traps where water can sit and smell. Where the pump is fitted to equipment that runs through load-shedding or on backup supply, the power arrangement has to be checked carefully so the pump starts when needed and does not overload the circuit.
We also look at the type of refrigerant system and the heat load around it. The pump itself does not use gas, but the surrounding cabinet or evaporator can be affected by poor airflow, blocked coils or a control fault. If the equipment is already running warm, the extra condensate load may point to a deeper issue with doors, seals, defrost timing or coil condition. In Gqeberha's coastal humidity, that can show up quicker than many people expect.
Installation usually includes a test run with water, a check of the float action and a visual inspection of the discharge route. Where space is tight, a careful neat install matters because access for later cleaning is often limited, and once the pump is boxed in it becomes a nuisance to service.
Care, servicing and fault signs to watch
Like most small mechanical parts, condensate pumps need periodic attention. Dirt, scale, food dust and algae can build up in the tank or the float area. If the pump is left unchecked, it can stick, run continuously, or fail to lift water when the unit defrosts. That can lead to overflow into the cabinet base or onto the floor.
Regular servicing keeps the pump reliable, especially on sites that see constant door opening or high ambient temperatures. During planned maintenance we check the inlet, clean the tank, confirm the float movement, test the discharge and inspect the electrical connections. On urgent callouts, we also look for blocked discharge lines, failed check valves and signs that the drain route is backing up.
- Water pooling under the fridge or evaporator
- Pump running but not discharging
- Intermittent alarms or overflow trips
- Bad smell from the drain tray or hose
- Visible algae, sludge or scale in the tank
What to check when ordering the right pump
To match the correct condensate pump, it helps to know the equipment type, the amount of water being moved and the route to the drain point. If you are replacing an old unit, take a photo of the nameplate and the existing hose path. If the site is new, measure the lift height in metres and the horizontal run, then check where the discharge will terminate. That saves time on site and reduces the risk of a wrong size being fitted.
It also helps to know whether the pump must sit inside a cabinet, under a counter, or in a service void with limited access. For food premises, ask whether the discharge can run to an approved waste point without crossing open product areas. In some buildings, municipal drainage rules or landlord requirements may also apply, so it is worth confirming before the install starts. A bit of checking upfront can prevent a messy redo later.
- Equipment type and model if available
- Required lift height in metres
- Approximate water volume and duty cycle
- Power supply available at the site
- Space available for tank, hose and maintenance access
Supply and support from our Newton Park base
Nvirocool supplies and supports condensate pumps for refrigerated cabinets, evaporators and compact cooling installations across Gqeberha, Uitenhage, Despatch, Jeffreys Bay, Graaff-Reinet and Port Alfred. From our Newton Park base, we help with selection, installation, testing and ongoing servicing, whether the job is a single pump changeout or part of a wider cold room maintenance visit.
Our team works on planned maintenance, emergency breakdowns, cold room repairs, chiller servicing, low-GWP conversions, leak detection, energy audits, coil cleaning, control upgrades and temperature monitoring. So if a pump failure is tied to a drainage issue, ice build-up or control problem, we can sort the full fault rather than only the symptom. For practical support, email hello@nvirocool.co.za and we will take it from there.
Key facts
| Product type | Condensate pump for refrigerated cabinets, evaporators and compact cooling systems |
|---|---|
| Typical discharge lift | Up to 3 m to 5 m depending on model and pipe route |
| Discharge connection | Usually 6 mm to 8 mm hose, with check valve where needed |
| Power supply | Commonly 220 V to 240 V AC single phase |
| Control | Float switch or sensor activated collection tank |
| Use conditions | Suitable for cold rooms, display cabinets, kitchens and service void installs |